
 Search


Trough chain conveyors / Screw conveyors
pdf | 815 KB
RUD H&E offers you a wide range of systems, installations and solutions that are specially customised to your individual requirements. We develop and manufacture reliable and powerful elevators, continuous conveyors, bucket elevators, chain conveyors and scraper chain conveyors based on the proven round steel chain as a means of traction.
Depending on the application, link chains or belt solutions are also used to ensure maximum efficiency and optimum operational safety. Our experienced engineers have extensive specialist and application knowledge and will support you as a competent partner in the development and realisation of your specific conveying task.
RUD H&E Service can also support you directly on site if required - from installation and conversions to maintenance of your system or machine.
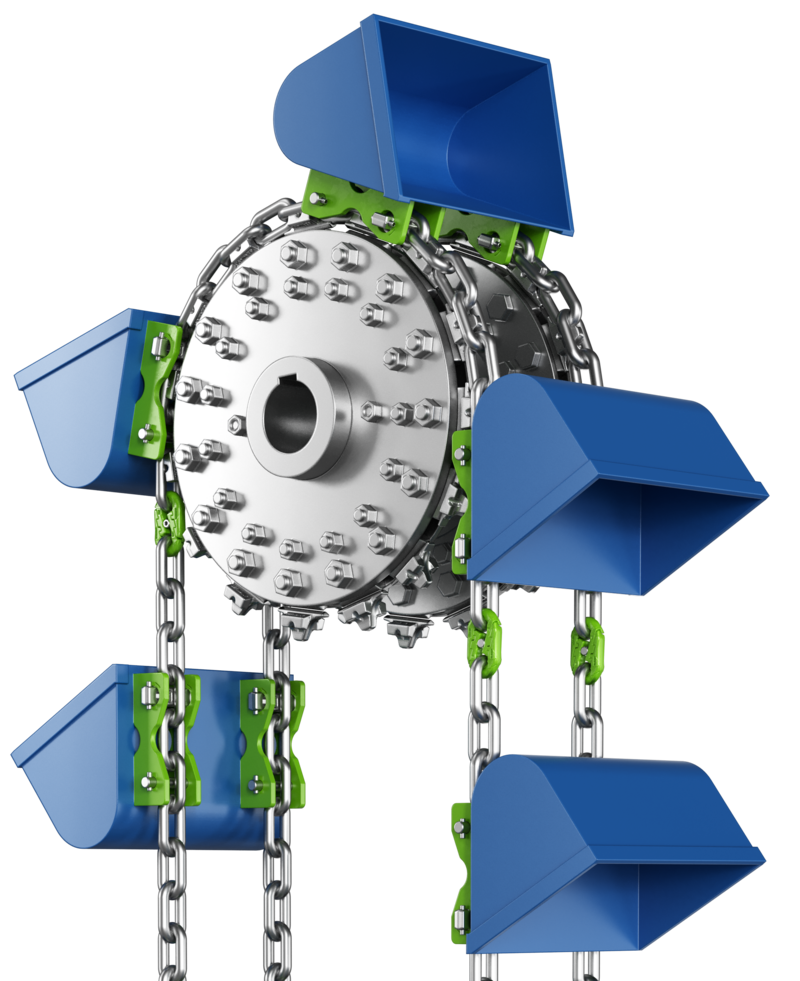
RUD H&E round steel chain bucket elevators and chain elevators are the proven solution for dust-free, vertical transport of powdery, granular, lumpy and temperature-loaded bulk materials.
Thanks to highly wear-resistant RUD chains and sprockets, safe and reliable operation is guaranteed even with abrasive materials. Depending on the application, our bucket elevators are available in various designs - for example with a constricted bucket strand or centre discharge design.
RUD H&E develops and manufactures complete central chain bucket elevators for the reliable and efficient transport of bulk materials.
Our systems are designed for use under demanding conditions - ideal for powdery, granular, lumpy or temperature-loaded materials. Thanks to the use of high-quality RUD central chains as traction equipment, our bucket elevators guarantee maximum operational reliability, even with abrasive materials, changing loads and high temperatures.
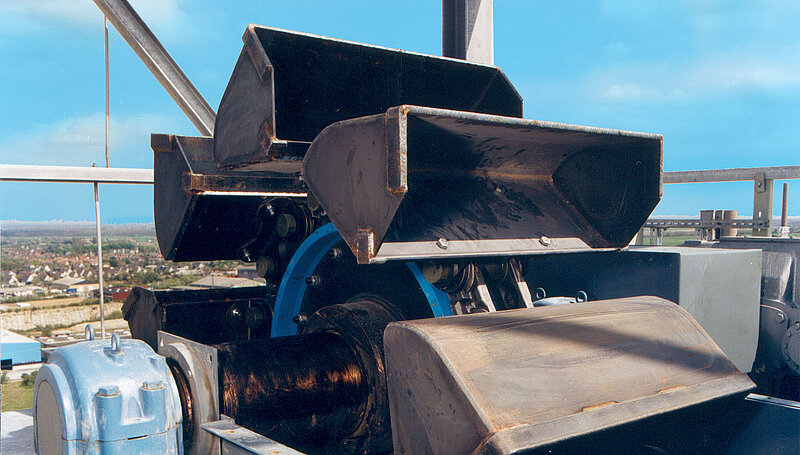
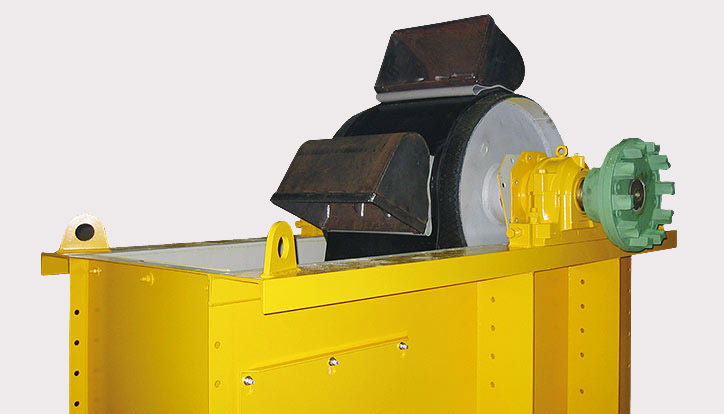
Belt bucket elevators / continuous conveyors or elevators are particularly suitable for the continuous vertical conveying of scoopable bulk materials. The elements for the elevator are selected depending on the properties of the material to be conveyed (whether coarse-grained or temperature-loaded, for example). Sturdy belts with fabric or steel inserts transport the material to be conveyed dust-free and without any problems, even over large bucket elevator conveying heights.
For dust-free, horizontal and slightly ascending conveying and dosing, even of coarse-grained bulk materials, trough chain conveyors are suitable as mechanical continuous conveyors with traction means. They are characterised by high wear and heat resistance and offer the option of integrating multiple inlets and outlets. Cleaning scrapers can also be supplied as a special design.
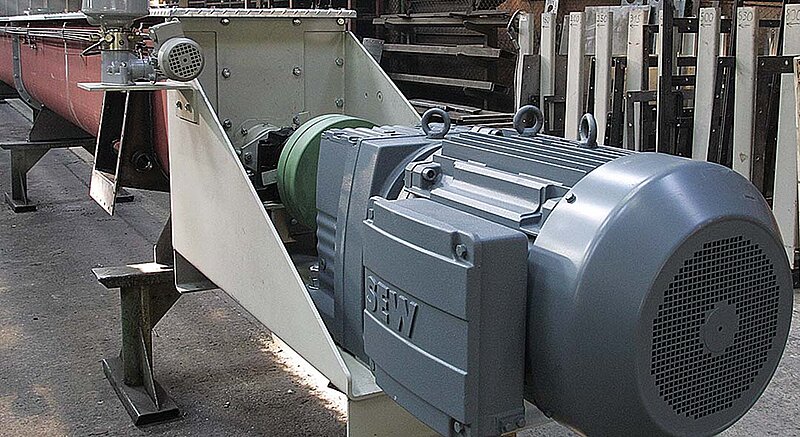
Screw conveyors are the ideal solution for the dust-free transport of fine-grained to floury bulk materials. They can be adapted to different material properties such as abrasiveness, temperature or flow behaviour and are available in various designs. Multiple inlets and outlets enable flexible application options - from conveying and dosing to mixing and cooling.


